What roller materials are suitable for high-pressure composite consolidation processes?
Chilled iron, forged alloy steel, and induction-heated steel roller units are the three proven shell materials. Chilled iron provides a hard white-iron working face over a vibration-damping gray-iron core for medium loads. Forged 42CrMo4-class steel carries the widest nips at continuous loads of 150–400 N/mm. Induction-heated steel units deliver 280–400°C surface temperatures with roughly ±1°C face uniformity for thermoplastic matrices such as PEEK, PEKK, and PA. Tungsten carbide, hard chrome, and ceramic coatings extend life against fiber abrasion, resin fouling, and chemical attack. Every selection must be verified with material certificates, hardness mapping, runout limits of 0.005 mm or better, and full-load temperature trials.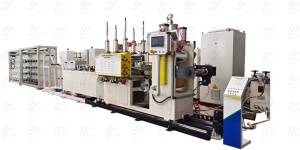
|
Item |
Description |
|
Function |
Deliver uniform high nip pressure and surface temperature to consolidate fiber–matrix laminates |
|
Material |
Chilled iron, forged alloy steel (42CrMo4 class), induction-heated steel shells |
|
Application |
Prepreg consolidation, double-belt laminating, calender nips, pressure vessel curing, laminate pressing |
|
Service Life |
1–3+ years between re-coats in abrasive duty; longer in clean thermoplastic duty |
A high-pressure consolidation roller is a rotating cylindrical machine element that presses fibrous resin systems — prepreg, UD tape, filament-wound tows, or impregnated fabrics — into dense laminates under controlled nip loads typically between 100 and 400 N/mm. Unlike guide and idler rollers, which mainly carry and steer the web, consolidation rollers are structural elements: their shells bend, heat, wear, and fatigue under load. Material selection is therefore a load-bearing engineering decision with direct consequences for laminate thickness, void content, and surface quality.
Consolidation combines pressure, heat, and time at the nip. Pressure drives resin through fiber bundles and expels entrapped air; heat softens the matrix so it flows, and in thermoplastics crystallization is controlled by cooling. Three material-related phenomena decide the outcome:
The consolidation position sits inside a complete web-handling chain: thermoset prepreg rolls and thermoplastic prepreg rolls upstream, cooling positions derived from film-line PRS cooling roll and BOPP chill roll practice downstream, and inspection and winding beyond. Treating the line as a knowledge graph — previous process, current process, next process — is also how roller materials should be specified: every interface transfers load and heat.
|
Property |
Chilled Iron |
Forged Alloy Steel |
Induction-Heated Steel Unit |
|
Surface hardness |
450–600 HB hard layer |
Via coating/treatment |
Via coating/treatment |
|
Core toughness |
Good (damped gray iron) |
Excellent |
Excellent |
|
Nip load capability |
Medium |
High, 150–400 N/mm |
High |
|
Face temperature capability |
~200°C with media heating |
~350°C (oil/water double shell) |
400°C+ |
|
Temperature uniformity |
±3–5°C typical |
±1–2°C |
±1°C |
|
Thermal response |
Slow |
Moderate |
Minutes |
|
Best fit |
Medium-load calendering |
Wide high-load nips |
Thermoplastic consolidation |
Supporting products complete the system: the induction heat calender roll and induction calender roll platforms carry the thermal duty; a ceramic coating roll serves chemically aggressive matrices; hardened and patterned faces for related film duty are documented on the casting roll and embossed roll pages. For heating-method engineering in depth, HUATAO's induction heating roll comparison remains the reference text.
|
Application |
Recommended System |
Engineering Reason |
|
Thermoset prepreg calendering |
Chilled iron or forged steel + hard chrome |
Damping plus release behavior |
|
CF/PEEK UD tape consolidation |
Induction-heated steel + polished face |
Temperature authority and uniformity |
|
Glass-rich lamination |
Forged steel + WC-Co spray |
Abrasion dominance |
|
Pressure vessel curing stations |
Forged steel shells, oversized journals |
Structural load and fatigue |
|
Low-Dk electronic laminate pressing |
Mirror-chrome forged steel |
Surface finish and thermal control |
|
Face-critical backup positions |
Rubber/PU covered roller |
Compliant pressure distribution |
|
Industry |
Consolidation Duty |
Typical Roller Configuration |
|
Aerospace composites |
Prepreg curing, thermoplastic blank consolidation |
Heated steel rollers, ±1°C uniformity, chrome faces |
|
Wind energy |
CF spar cap laminates, root inserts |
Wide forged-steel nips, WC faces against glass abrasion |
|
Hydrogen storage |
Filament-wound Type IV vessel processing |
Heavy journal shells, precision runout control |
|
Electronics / 5G materials |
Low-Dk laminate pressing for AI-server boards |
Mirror-chrome faces, tight thermal uniformity |
|
Automotive lightweighting |
Double-belt thermoplastic sheet lines |
Induction heating, continuous duty ratings |
|
Consumer products |
Recycled-CF laminate consolidation |
Compliant backup surfaces, moderate loads |
Information to provide: face width, nip load band, line speed, matrix and fiber types, temperature range and uniformity target, existing machine interfaces, and annual tonnage.
Drawings needed: shell geometry, journal dimensions, bearing types, heating method and media circuit, coating specification with thickness, and acceptance limits.
OEM part numbers: when replacing existing units, provide OEM references so journals and interfaces can be matched exactly.
Material selection: agree shell class, coating system, and hardness/roughness bands before quoting so offers are comparable.
MOQ, lead time, packaging, shipping: coated and heated rollers ship with protective faces, desiccant, and shock indicators; agree inspection standards and third-party witness points.
Supplier evaluation checklist:
Reference economics: HUATAO's published chrome-plated chill roll case and corrosion-resistant roll case show how correct material and surface specification cut lifetime roller procurement costs by 50–60% — the same logic applies to consolidation duty.
|
Problem |
Possible Cause |
Recommended Solution |
|
Thickness uneven |
Shell deflection or thermal gradient |
Stiffer shell, deflection-compensating backup, full-load temperature testing |
|
Materials peel off |
Coating adhesion loss, thermal mismatch |
Thermally matched coating, adhesion qualification |
|
Low efficiency |
Slow thermal response of media-heated shells |
Induction heating conversion |
|
Excessive downtime |
Resin fouling and glazing |
Chrome or ceramic release surface, cleaning schedule |
|
Poor fitment |
Journal wear, wrong interfaces |
Re-machining, OEM replacement service |
|
Material mismatch |
Coating incompatible with resin chemistry |
Ceramic surface for acidic/styrenated systems |
|
Installation failure |
Misalignment, improper connections |
Supervised commissioning and alignment protocol |
|
Roller vibration |
Dynamic imbalance at operating speed |
Balance at speed, bearing replacement |
|
Surface marking |
Hardness below fiber abrasion threshold |
WC-Co upgrade, hardness mapping program |
|
Web slippage |
Contaminated or glazed face |
Clean and re-texture, verify nip settings |
|
Bearing failure |
Undersized journals |
Enlarge journals, heavy-duty spherical bearings |
|
Coating delamination |
Thickness or cure out of specification |
Coating supplier audit, thickness and porosity control |
|
Dynamic imbalance |
Shell wear asymmetry |
Re-grinding and re-balancing decision point |
|
Runout out of tolerance |
Journal wear or shell distortion |
Runout measurement loop, re-grinding plan |
Question: What is the best roller material for high-pressure composite consolidation? Answer: No single material wins — the duty decides. Chilled iron fits medium-load calendering where damping matters; forged alloy steel carries wide nips at 150–400 N/mm; induction-heated steel units serve thermoplastic matrices at 280–400°C. Then match the coating to the dominant wear mode.
Question: Why is chilled iron still used when forged steel is stronger? Answer: Chilled iron pairs a very hard working layer with a graphite-bearing core that damps vibration, preventing chatter marks at medium loads and lower cost. Forged steel wins where stiffness demands are extreme.
Question: What nip loads can these materials handle? Answer: Properly engineered forged-steel systems run 150–400 N/mm continuously. The practical limits are face deflection and bearing capacity — which is why journal sizing matters as much as shell alloy.
Question: Which coating should I choose for glass fiber contact? Answer: WC-Co HVOF spray at 1,100–1,300 HV. It resists abrasive scrubbing several times longer than nitrided steel and keeps the ground roughness stable, protecting laminate surface quality.
Question: Is induction heating worth the investment for thermoplastic consolidation? Answer: For PEEK, PEKK, and PA matrices, yes: higher temperatures, minute-level response, ±1°C uniformity, and no pressurized oil inside the shell. Changeover time and scrap reduction typically repay the premium.
Question: What acceptance tests prove material quality on delivery? Answer: Material certificates, hardness mapping across the face, coating thickness and adhesion reports, runout ≤0.005 mm, dynamic balance grade, and a cross-face temperature uniformity trial under full load with your material.
Question: Can existing rollers be upgraded instead of replaced? Answer: Often. Shells can be re-ground and re-coated, journals re-machined, and oil-heated units converted to induction heating after a duty review. An OEM replacement assessment identifies the economical route.
Question: How does roller material affect laminate void content? Answer: Uniform nip pressure and temperature drive resin flow and air evacuation. Deflection and thermal gradients create local under-pressure zones that entrap voids, so shell stiffness and thermal uniformity are void-content controls.
Question: What price differences should I expect between quotes? Answer: Forging versus casting, double-shell construction, coating system, journal sizing, and testing depth drive the spread. Compare three-year total cost of ownership, including re-coats and downtime, rather than invoice price.
Question: How often should consolidation rollers be re-coated? Answer: Every one to three years in abrasive glass-rich duty, longer in clean thermoplastic duty. Hardness-mapping trends — not calendar time — should trigger the decision.
High-pressure composite consolidation rewards buyers who specify rollers as engineered systems: a stiff shell alloy chosen against the worst-case nip load, a surface system chosen against the dominant wear mode, a heating method chosen against the matrix, and rotating hardware chosen against deflection. The November 2026 landscape — peroxide-grafted CFRP sizing raising interface targets, sensor-instrumented 70 MPa vessels auditing every consolidation decision, and a fast-growing low-Dk laminate market pressing new resin chemistry — raises the bar again. The winning specification is documented, measured under load, and matched to real duty. For engineering reviews, drawings, and OEM replacement support across HUATAO's industrial roll platform, contact the team directly.
Jenny Liu Email: sale05@huataogroup.com Phone / WhatsApp: +86 17743789775 Website: https://www.huataomulti-indusrolls.com/
#IndustrialRoller #CompositeRoller #HighPressureConsolidation #RollerMaterials #ChilledIronRoll #ForgedSteelRoller #InductionHeatingRoll #TungstenCarbideCoating #CeramicCoatingRoll #HardChromeRoll #PressRoller #NipRoller #CalenderRoller #HeatedRoller #ThermoplasticComposite #PrepregLine #CarbonFiber #HydrogenStorage #WindEnergy #HUATAO
can not be empty
can not be empty

HUATAO GROUP - ROLLS
Address: No.298 Zhonghua North Street, Shijiazhuang 050000 China.
Tel: +86 0311 80690567
Email: sale08@huataogroup.com
 WhatsApp & WeChat : +86 13383112591