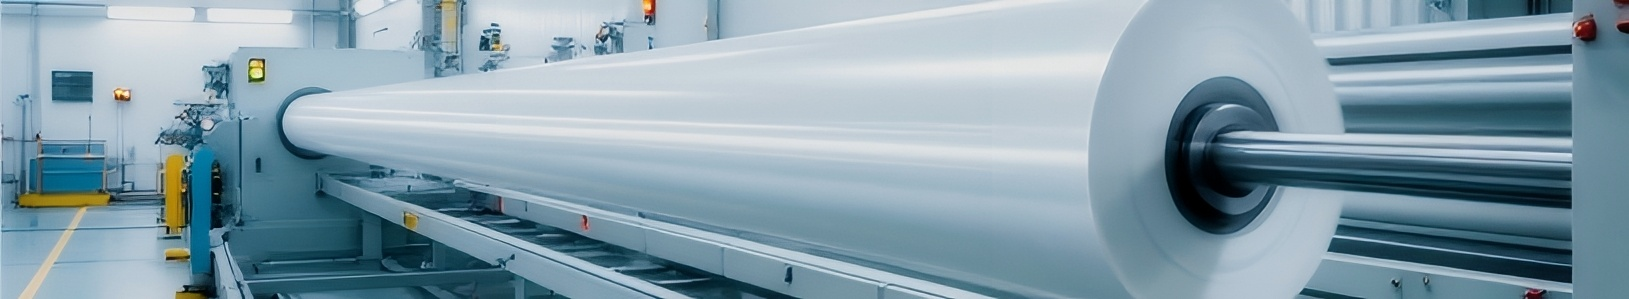
In cast plastic film extrusion, the cooling section plays a central role in converting a molten polymer web into a stable film. Two terms frequently appear in equipment specifications and technical discussions: casting roll and chill roll. Although they are closely related, they do not always describe the same position in the production line.
A casting roll generally refers to the first major roll that receives the molten polymer after it exits the flat die. It establishes the initial contact and cooling conditions. A chill roll is a broader functional term for a temperature-controlled roll that removes heat from the film. The first casting roll is therefore also a chill roll by function, while additional chill rolls may be positioned downstream to continue cooling.
The terminology varies among equipment manufacturers and production plants. Some use “primary chill roll” and “casting roll” to describe the same component; others distinguish the casting roll from the subsequent cooling rolls.
For engineers, maintenance teams, and purchasing managers, the most important issue is not the name alone. It is the roll's position, function, thermal requirements, surface characteristics, and compatibility with the complete extrusion line.
A typical cast film extrusion line begins with polymer melting and plasticization in the extruder. The melt passes through filtration and, where applicable, a feedblock before reaching the flat die. The die forms the melt into a wide, thin curtain that travels toward the primary roll.
The casting roll is normally positioned close to the die. The molten web is brought into contact with its surface and begins to cool.
Initial film contact
The first contact between the molten polymer and the casting roll is important. The film must be laid down consistently across the working width. Depending on the line design, an air knife or vacuum box may assist this contact by pressing the melt toward the roll or removing air from the interface.
Initial heat removal
The casting roll transfers heat away from the molten polymer. Its cooling capacity must be compatible with the resin, film thickness, production speed, and required process conditions.
Film stabilization
As the polymer cools, the web becomes more stable for downstream handling. The casting roll therefore participates in both thermal management and initial film formation.
Surface replication
The roll surface can influence the appearance of the film surface that contacts it. A highly polished finish may be specified for certain optical requirements, while other products may require a different surface texture or finish. The required surface must be defined by the film specification and equipment design.
Because of these functions, the casting roll is a process-critical component rather than a simple transport roller.
The term chill roll describes a roll that removes heat from a moving web or material. In cast film extrusion, the first casting roll performs this function, but the cooling section may also include additional rolls.
Primary chill roll
The primary chill roll is usually the roll directly below or near the flat die. In many lines, it is the same component referred to as the casting roll. It receives the molten film and provides the first major stage of contact cooling.
Downstream chill rolls
Additional chill rolls may be used to continue removing heat from the film. Their role is to bring the film toward the temperature required for subsequent operations, which may include thickness measurement, edge trimming, surface treatment, stretching, or winding.
Cooling-roll sequence
The number, diameter, arrangement, surface finish, and temperature settings of the rolls depend on the line design. Some systems use a relatively simple cooling arrangement, while others use several rolls to manage heat removal and film handling.
The important distinction is therefore:
A casting roll normally identifies the primary roll receiving the melt from the die.
A chill roll identifies a cooling function and may refer to the primary roll or a downstream roll.
A primary casting roll can be described as a primary chill roll, but a downstream chill roll is not necessarily the casting roll.
This distinction is useful for technical communication, but the equipment manufacturer's terminology and drawing should always be checked before a replacement is ordered.
Casting and chill rolls work as part of an integrated process. Their performance depends on the relationship between the die, polymer, air gap, roll surface, cooling system, and downstream web path.
Polymer type and melt behavior
Different polymers have different processing temperatures, crystallization behavior, and cooling requirements. Resin grade, additives, melt temperature, and film structure can influence how the film responds to the cooling section.
A roll specification should therefore be evaluated against the actual polymer and film product rather than a generic cast film temperature.
Film thickness and production speed
Film thickness and line speed affect the amount of heat that must be removed. A higher production rate can change the cooling demand and the time available for heat transfer. The required cooling configuration must be considered as part of the overall line design.
Cooling-water system
The roll's internal cooling arrangement, water flow, inlet temperature, outlet temperature, and temperature distribution can influence heat transfer. Internal deposits or restricted passages may affect cooling performance. Maintenance and water-quality management should follow the equipment requirements.
Surface finish and cleanliness
The roll surface may transfer its finish to the film. Scratches, deposits, contamination, or damage can create visible defects. Cleaning procedures should be suitable for the roll surface and should avoid damaging precision-finished areas.
Alignment and film contact
The relationship between the flat die, primary roll, pressure or nip components, air knife, and vacuum system can influence film contact. Poor alignment or unstable contact may contribute to wrinkles, air entrapment, uneven cooling, or inconsistent surface quality.
Temperature uniformity
A stable cooling process requires appropriate temperature control across the roll and through the cooling sequence. The correct temperature settings depend on the resin, film thickness, line speed, and equipment design. A single temperature recommendation should not be treated as universal.
When film quality changes, the casting roll or chill roll may be one of several possible factors. A systematic investigation should consider the complete process.
Wrinkles or unstable laydown
Possible factors include die alignment, roll alignment, web tension, air-knife settings, vacuum performance, and uneven contact. Check the film path and the relationship between the die and the primary roll.
Air entrapment and surface defects
Air between the molten web and the roll can interfere with heat transfer and contact. Inspect the air knife or vacuum system, roll surface, and operating settings. The defect pattern may help determine whether the issue is localized or across the full web width.
Uneven cooling
Potential causes include variations in cooling-water flow, temperature, internal deposits, or changes in production speed and resin conditions. Check the cooling circuit and compare temperatures across the roll face where measurement is available.
Scratches and marks
Inspect the roll surface for damage, contamination, and deposits. Review cleaning tools and procedures, as inappropriate maintenance can damage a polished working surface.
Sticking or difficult film release
Possible factors include resin behavior, surface condition, process temperature, contact conditions, and downstream web handling. Review the process before assuming that a different roll surface is required.
Vibration or abnormal noise
Check bearings, shaft interfaces, alignment, mounting, balance, and operating speed. Confirm runout and balancing requirements against the machine specification.
A defect should not be attributed to the roll without evidence. The die, resin, extruder output, cooling circuit, air knife, vacuum system, and web-handling settings may all contribute.
What information should be provided for a casting roll or chill roll quotation?
A complete technical request should identify the roll's position and function, then provide the dimensional and process information needed for evaluation.
Machine manufacturer, model, and line configuration
Roll position: primary casting roll or downstream chill roll
Roll diameter, face length, overall length, and shaft dimensions
Core structure and wall thickness, where applicable
Existing drawing, OEM part number, or verified sample
Polymer type, film structure, thickness, and working width
Line speed, melt conditions, and operating temperature
Cooling-water inlet and outlet requirements, flow, and temperature
Surface finish, roughness, and any special texture
Runout, concentricity, balance, and dimensional tolerances
Inspection documents, acceptance criteria, packaging, and delivery requirements
For a replacement roll, shaft ends, journals, bearing seats, drive connections, and installation clearances should be confirmed. Similar external dimensions do not guarantee interchangeability.
Frequently Asked Questions
1. Are chill roll and casting roll two different types of equipment?
They may refer to different positions in the line, but the terminology overlaps. The casting roll is generally the primary roll receiving molten film from the die. Chill roll is the broader functional term for a roll that removes heat.
2. Is the first chill roll also called a casting roll?
Yes. In many cast film lines, the first chill roll is also called the casting roll, casting drum, or primary chill roll.
3. What is the main function of a casting roll?
It receives the molten polymer web after the flat die, removes heat, and helps establish initial film contact and stabilization.
4. Why are additional chill rolls used?
They can provide further heat removal and help bring the film to a suitable temperature for downstream measurement, trimming, treatment, or winding.
5. Does the casting roll determine film thickness?
Film thickness is influenced by several factors, including die settings, melt output, drawdown, roll speed, and process control. The casting roll is part of the process, but it does not independently determine final thickness.
6. Does casting-roll surface finish affect the film?
Yes. The surface in contact with the polymer can influence the corresponding film surface. The appropriate finish depends on the product's appearance and functional requirements.
7. What is the purpose of an air knife?
An air knife may help press the molten web against the casting roll to improve contact. Its configuration and settings depend on the extrusion line.
8. What is the purpose of a vacuum box?
A vacuum box may remove air from the contact interface and help stabilize film laydown on the casting roll.
9. How can I identify whether a problem comes from the casting roll or the cooling system?
Review roll-surface condition, alignment, runout, temperature distribution, cooling-water flow, and film-contact behavior. Also inspect the die, air knife, vacuum system, and process settings before assigning a root cause.
10. What is the most important information when ordering a replacement roll?
Confirm its exact position and function, approved drawing, dimensions, shaft interfaces, surface finish, cooling requirements, operating conditions, and inspection criteria.
Related HUATAO Products
Explore Chill Roll and the wider Polyfilm Line Rolls category. Other film-processing roll categories include PRS Cooling Roll, MDO Preheating Roll, and MDO Stretching Roll.
Contact HUATAO
Contact: Tony Liu
Email: sale08@huataogroup.com
Phone / WhatsApp: +86 13383112591
Website: https://www.huataorolls.com/
HUATAO welcomes inquiries from customers worldwide. Send your roll drawing, line configuration, polymer and film details, operating conditions, and inspection requirements to discuss your project.
can not be empty
can not be empty

HUATAO GROUP - ROLLS
Address: No.298 Zhonghua North Street, Shijiazhuang 050000 China.
Tel: +86 0311 80690567
Email: sale08@huataogroup.com
 WhatsApp & WeChat : +86 13383112591